
Applying ROPP Caps: Roll-On Capping, Torque and Tamper Evidence
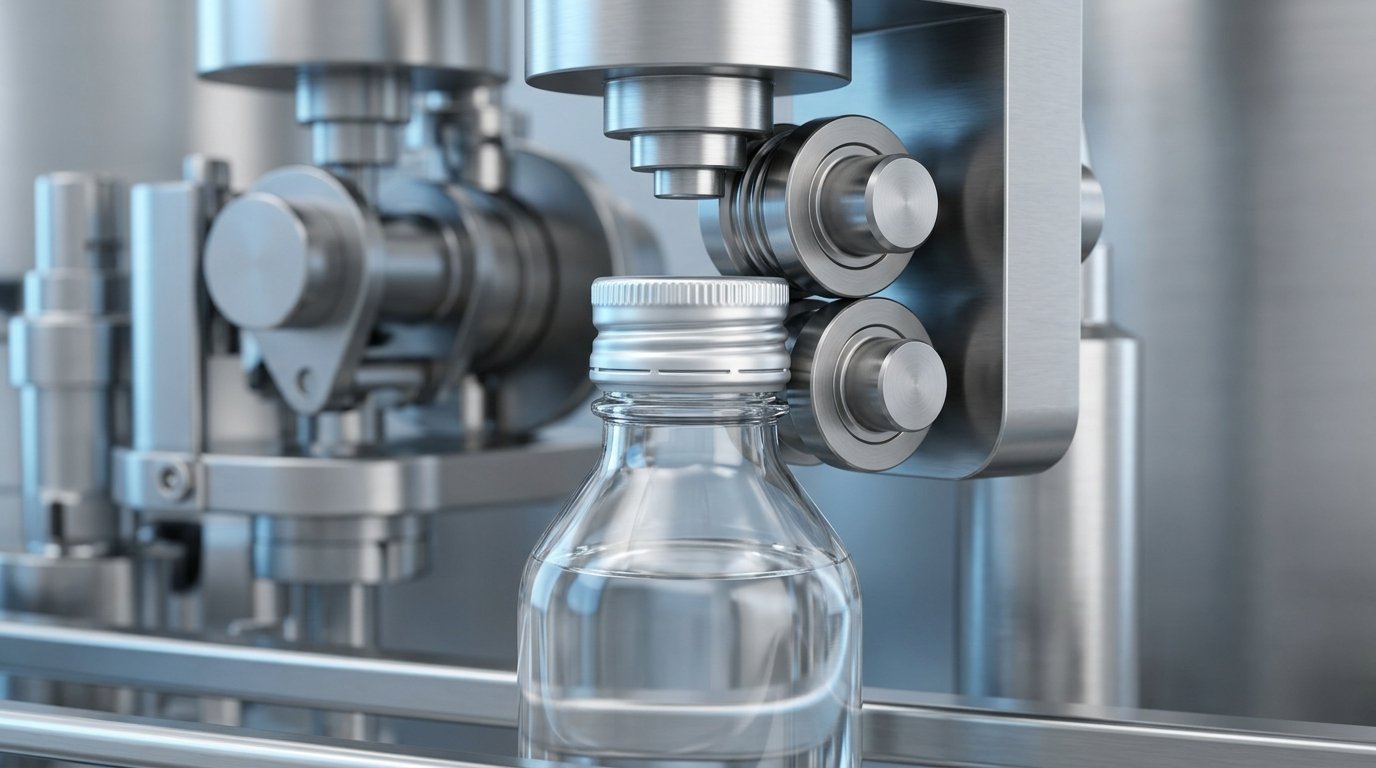
A pilfer-proof cap is applied by roll-forming, not by screwing. The threadless aluminium shell is placed over the bottle neck and held down under top load while thread rollers press the soft metal into the bottle’s own thread profile, and a separate pilfer roller tucks the lower band under the retaining bead. The threads are therefore created against the specific bottle at the moment of capping. That is what makes the fit tight and the tamper evidence irreversible, and it is also why capping-head setup is a validated parameter rather than a machine setting.
This page covers the capping sequence, the parameters that control it, how application and removal torque behave, how the pilfer band delivers tamper evidence, and the defects that show up when a setting drifts.
Key takeaways
- ROPP stands for roll-on pilfer-proof, and it describes the application method: threads are rolled onto the bottle, not moulded into the cap.
- The cap is delivered as a smooth threadless shell with a liner inside, a knurled skirt and a lower band joined to the body by thin bridges.
- Capping does two jobs at once: thread forming by the thread rollers and band tucking by the pilfer roller.
- The controlling parameters are top load, roller pressure, roller position and head speed, all re-established at a size or profile changeover.
- Tamper evidence is mechanical and one-time. The band cannot lift over the bottle bead, so on first opening the bridges shear and the band stays behind.
- The cap remains reclosable on its formed threads; only the tamper evidence is single-use.
- Most capping defects trace back to top load, roller setting or a cap-to-neck mismatch, which is why cap dimensional consistency matters to line performance.
The roll-on capping sequence
Roll-on capping happens in one continuous head cycle, and the whole closure is formed in that cycle. In sequence:
- Feed and place. Caps are fed from a sorter down a chute and placed over the bottle neck. Because the shell is threadless and symmetrical, no angular orientation is required, which is one reason ROPP lines run fast.
- Apply top load. A knockout or pressure block presses down on the crown of the cap. This seats the liner against the bottle’s sealing land and holds the shell square while the metal is worked. Top load is what creates the seal; the threads only hold it.
- Form the threads. Two or more thread rollers move in against the skirt and iron the aluminium into the bottle’s thread profile as the head and bottle rotate relative to each other. The metal takes the shape of the glass or plastic beneath it.
- Tuck the pilfer band. A separate pilfer roller presses the lower edge of the skirt inward, under the retaining bead on the neck. The band is now captured below the bead.
- Release. The rollers retract, top load is removed, and the formed cap holds the liner in compression on its new threads.
At the end of the cycle the closure is a screw cap with a captive band. It can be unscrewed and rescrewed like any other screw cap, but the band cannot travel back over the bead, so the first opening breaks the bridges.
Why the threadless approach helps
Forming the threads against the actual bottle removes the tolerance stack that a pre-threaded cap has to absorb. A moulded screw cap has to fit a population of bottles whose necks vary within their own tolerance band, so the thread engagement varies bottle to bottle. A rolled cap takes the shape of the neck in front of it.
The practical effects are a consistent thread engagement, a band that sits tight under the bead, and a seal that depends more on top load and liner behaviour than on how the two thread forms happen to mate. The trade-off is that the closure is created on the customer’s line rather than delivered finished, so line setup carries responsibility that a pre-threaded closure would carry in the mould. Autofits positions the range on that basis, describing the caps as offering good machinability and helping maintain closure integrity.
The parameters that control the result
Four settings do most of the work, and all four are re-established when the size or the cap profile changes.
| Parameter | What it controls | What happens if it drifts |
|---|---|---|
| Top load | Liner compression and squareness of the shell | Too low: weak seal, shallow threads. Too high: stressed bottle finish, distorted crown |
| Thread roller pressure | Depth and definition of the formed threads | Too low: shallow threads that strip. Too high: thinned or cut metal |
| Pilfer roller position and pressure | How far the band is tucked under the bead | Too low: band lifts over the bead and tamper evidence fails. Too high: band breaks during application |
| Head and bottle speed | Number of forming passes per cycle | Too fast: incomplete forming. Too slow: over-worked metal and throughput loss |
A size change, for example from a 28 mm to a 38 mm cap, means a changeover of the head parts and a re-establishment of all four. A change from a square shoulder to a chamfered profile is smaller but still confirmed on the line rather than assumed.
Application torque and removal torque
Application torque is not a directly set parameter on a roll-on capper the way it is on a screw capper. There is no torque clutch tightening a pre-threaded cap; the closure’s tightness is a product of top load and how completely the threads were formed. What the line measures is the result.
- Removal torque is the practical control. It is measured on capped units, after any conditioning the pack will see, and it has to sit in a window: high enough that the pack does not loosen in distribution, low enough that the intended user can open it. That window is set per pack during qualification.
- Torque decay over time is normal as the liner relaxes, which is why removal torque is measured after conditioning and not only straight off the line.
- Leak testing on filled, capped units is run alongside torque, because a cap can be within the torque window and still leak if the liner is wrong for the product or the sealing land is damaged. Liner selection is covered on the ROPP cap liners page.
How the pilfer band delivers tamper evidence
The tamper evidence is geometric. The band is smaller than the bead it sits under, so it physically cannot travel back up the neck. When the cap is unscrewed, the cap body rises on its threads while the band stays trapped. The thin bridges connecting the two shear, and the band either stays on the neck or hangs loose. There is no way to reattach it and no way to re-form it without recapping equipment.
That is why the feature is described as pilfer-proof rather than merely tamper-resistant: the evidence is created by the act of opening, not by a label or a shrink sleeve that could in principle be replaced. A missing or broken band is visible to a pharmacist or a patient before the product is used, which is the point of the design. The wider context of falsified and substandard medicines, and why visible closure integrity matters to it, is set out by the World Health Organization.
In the United States, tamper-evident packaging for over-the-counter human drug products is a regulatory requirement rather than a design preference. 21 CFR 211.132 requires such products to be in a tamper-evident package, defined as one having one or more indicators or barriers to entry which, if breached or missing, can reasonably be expected to provide visible evidence to consumers that tampering has occurred, and each retail package has to carry a prominent statement identifying the tamper-evident feature. A correctly tucked pilfer band is one of the closure-level ways of meeting that intent; the applicable requirements for a specific product and market are confirmed with the regulatory group. The general regulation is discussed on the 21 CFR Part 211 page, and the equivalent thinking for injectable vials on the tamper-evident vial closures page.
Common capping defects and what they mean
Most defects on a ROPP line point back to one of the four settings, or to a mismatch between the cap and the neck.
| Defect | Usual cause |
|---|---|
| Cap spins freely, no thread engagement | Thread roller pressure too low, or wrong cap size for the neck |
| Band already broken at the capping head | Pilfer roller pressure too high, or band tucked against a damaged bead |
| Band lifts over the bead on first opening | Pilfer roller position too low, insufficient tuck |
| Leaking pack within torque spec | Liner unsuitable for the product, or damaged sealing land on the bottle |
| Crown deformed or dished | Top load too high |
| Threads formed but shallow and stripping | Top load too low, or head speed too fast for the passes required |
| Scuffed or marked outer surface | Roller condition, or feeding chute contact on a printed cap |
Two of these are the cap supplier’s responsibility rather than the line’s: dimensional consistency shell to shell, and clean, burr-free cut edges from the punching operation. Both are inspected before the caps leave the plant.
What the cap supplier controls
A closure that arrives dimensionally consistent, clean and free of burrs is the precondition for a stable capping line. The controls that matter upstream are:
- Dimensional consistency across a lot, so the head does not have to accommodate a moving target.
- Clean cut edges, so the rollers do not catch and so no metal fines are generated at the head.
- Consistent metal temper and lacquer, so the metal forms the same way from lot to lot.
- Inspection of the running output rather than sampling alone, so an intermittent defect does not reach the line.
- Clean, closed packing, so dust and fibres are not introduced at the capping station.
What a filling line needs to run ROPP caps
A line needs five things in place before the first production run: the right heads, the bottle drawing, trial caps, a way to measure removal torque, and a leak test.
- A roll-on capper with change parts for the size. Each cap size needs its own knockout or pressure block, thread rollers and pilfer roller set to the neck. Adding a size is a change-parts order, not only a new cap order.
- The bottle neck finish drawing, shared with the cap supplier. The cap drawing is built against it, and a second bottle source needs its own check.
- Trial caps in the production liner and finish. Settings found with a different liner or a plain cap do not transfer to a printed or chamfered one. Standard samples are typically 200 to 500 pieces per size.
- Removal torque measurement on capped units, straight off the line and after conditioning, against the window set during qualification.
- Leak testing on filled, capped units, since a cap inside the torque window can still leak.
Line speed is fixed last. The trial finds the head and bottle speed that forms complete threads and a clean band tuck with the chosen cap, liner and bottle, and that speed is then held; the capping machine maker’s rating sets the ceiling.
How this works in practice at Autofits
Autofits pilfer-proof caps are produced at the 75,000 sq ft facility in Nashik, India, which makes around 250 million of them a month, from AA8011 aluminium with an epoxy lacquer coating conforming to 21 CFR 175.300, and with online high-speed camera inspection. On a customer’s line, what that output has to deliver is the shell-to-shell consistency and edge quality described above, lot after lot.
Production sits under ISO 9001:2015, ISO 14001:2015 and ISO 15378:2017 with a Drug Master File (DMF 18100) and CFDA registration; the quality system standard is described on the ISO 15378 page and the certification set is on the quality page. Where a line is being set up or a size added, send the bottle neck finish drawing with the enquiry so the cap drawing supplied with the quotation matches the neck the caps will actually be rolled onto.
Frequently asked questions
How is a ROPP cap applied?
A roll-on pilfer-proof cap is applied by forming, not by screwing. The threadless aluminium shell is placed over the bottle neck and held under top load while thread rollers press the metal into the bottle’s own thread profile and a pilfer roller tucks the lower band under the retaining bead. The threads are created against that specific bottle during capping, which is what gives the closure its tight fit and its captive tamper-evident band.
What equipment is needed to apply pilfer-proof caps?
A roll-on capping machine with forming heads set up for the cap size and bottle neck finish. The head carries a knockout or pressure block for top load, thread rollers and a pilfer roller. Ordinary screw-capping equipment cannot apply a ROPP cap, because there are no threads on the delivered shell for a torque chuck to engage.
What is the correct application torque for a ROPP cap?
Roll-on capping does not set application torque directly the way a screw capper does; tightness results from top load and how completely the threads are formed. The controlled measurement is removal torque on capped units after conditioning, held within a window agreed during pack qualification: tight enough to survive distribution, loose enough for the intended user to open. The window is specific to the pack and is not transferable between products.
Why is the pilfer band breaking during capping?
Usually the pilfer roller pressure is set too high, or the roller is positioned so it works the band against a damaged or out-of-tolerance neck bead. Check the roller setting first, then the incoming bottle finish. If the band is intact at the head but lifts over the bead on first opening, the opposite fault applies: the tuck is insufficient.
Can a pilfer-proof cap be reclosed after opening?
Yes. Because the threads are formed onto the bottle during capping, the cap unscrews and screws back on like any other screw cap, and the liner reseals the container. The tamper evidence is single-use: once the bridges have sheared on first opening, the band stays broken and cannot be reattached, so the pack remains visibly opened even though it is reclosable.
Does the cap supplier affect capping line performance?
Yes, mainly through dimensional consistency and edge quality. A lot of caps that varies shell to shell forces the head to accommodate a moving target, and burrs left from punching can catch on the rollers and generate metal fines at the capping station. Consistent temper and lacquer, clean cut edges and inspection before despatch are what a supplier contributes to a stable line.
Related reading
- Pilfer-proof (ROPP) aluminium caps: the full range
- 22 mm, 25 mm, 28 mm, 35 mm and 38 mm ROPP caps
- ROPP cap liners: EPE, latex and PVC
- ROPP cap finishes: plain, printed and chamfered
- Crimp vs screw vial closure
- 21 CFR Part 211: GMP for finished pharmaceuticals
- Tamper-evident vial closures
Sources
- Autofits pilfer-proof (ROPP) cap range and product dossier (working/spec-sheets/)
- eCFR: 21 CFR 211.132, Tamper-evident packaging requirements for over-the-counter (OTC) human drug products (https://www.ecfr.gov/current/title-21/chapter-I/subchapter-C/part-211/subpart-G/section-211.132)
- eCFR: 21 CFR 175.300, Resinous and polymeric coatings (https://www.ecfr.gov/current/title-21/chapter-I/subchapter-B/part-175/subpart-C/section-175.300)
- World Health Organization: Substandard and falsified medical products (https://www.who.int/health-topics/substandard-and-falsified-medical-products)
- ISO: ISO 15378:2017, Primary packaging materials for medicinal products, GMP requirements (https://www.iso.org/standard/70729.html)
*Last updated: 2026-09-15. This page is general technical and product information, not regulatory or compliance advice; confirm current standard editions, your own market’s tamper-evidence requirements and your own specification with Autofits and the issuing bodies.*
