
Vial Closure Integrity: What It Means, How to Specify It and How It Is Tested
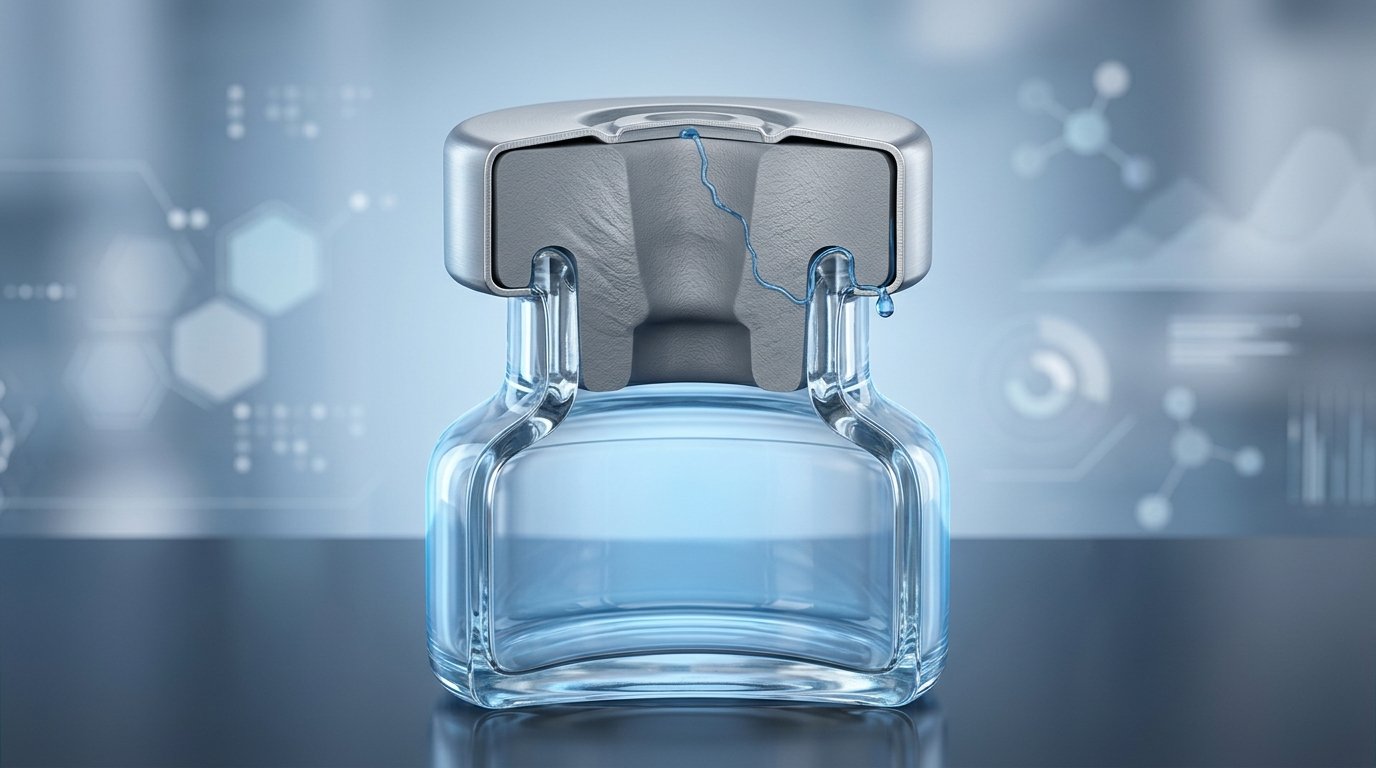
Vial closure integrity, more formally container closure integrity (CCI), is the ability of a sealed vial to keep its contents in and microorganisms, air and moisture out for its whole shelf life. It comes from three parts acting as one barrier: a rubber stopper held compressed against the glass by a correctly crimped aluminium seal, on a vial neck of the same nominal size, with no leak path between them. It is demonstrated by container closure integrity testing chosen and validated within the framework of USP <1207>.
Integrity is a property of the whole package rather than of any one component, and it is what keeps a sterile product sterile after it is sealed. This guide explains what closure integrity means, what the crimp, the stopper and the seal each contribute, what a buyer has to specify to get it, what can go wrong, and how integrity is tested.
Key takeaways
- Container closure integrity (CCI) is the sealed package’s ability to keep contents in and contaminants and microbes out for the shelf life.
- Integrity depends on the stopper held compressed against the glass by a correctly applied crimp; the seal holds the barrier, the stopper is the barrier.
- A too-loose or too-tight crimp can leave a leak path or damage the stopper, both of which are integrity failures.
- Integrity is specified, not just tested: the vial neck, the stopper, the seal and the capping settings have to be defined together as one vial closure system.
- The stopper compound matters as much as its size, because hardness and compression set decide how much sealing load remains over the shelf life.
- The seal contributes crimp geometry, aluminium gauge (0.16 to 0.25 mm across the flip-off range) and piece-to-piece dimensional consistency, verified by 100% high-speed camera inspection.
- It is evaluated within the framework of USP <1207> and demonstrated by container closure integrity testing (CCIT).
What container closure integrity means
Container closure integrity is the property of a sealed package that keeps the product in and keeps air, moisture and microorganisms out, continuously, until the vial is used. It is not the same as simply being “closed”. A vial can look closed and still have a microscopic leak path that lets in microbes or lets out headspace gas.
For a sterile injectable, integrity is a patient-safety attribute: if the package loses integrity, the product can be contaminated or degrade, and there is usually no way to re-sterilise it. For a cytotoxic oncology product it is an occupational-safety attribute too, because a leak path lets hazardous drug out as well as contamination in. Integrity is therefore designed into the container closure system, the glass vial with its matched stopper and crimped aluminium or aluminium-plastic seal, and then demonstrated by testing. It has to hold not just at sealing but through storage, transport, any temperature excursions the product sees and, for a multi-dose presentation, repeated needle entries. For vaccines and other cold-chain products that includes the strain of refrigerated or frozen storage on the seal and stopper interface.
Why the crimp is central to integrity
The crimp is central to integrity because it is what holds the rubber stopper compressed against the glass, and that compression is the seal. The stopper is an elastomeric closure: it deforms slightly when pressed onto the vial and, held in compression, it fills the microscopic gaps at the glass interface to close any leak path.
The aluminium seal’s job is to apply and maintain that compression. During capping, the lower skirt of the seal is rolled under the vial neck flange, drawing the stopper down and locking it there. If the crimp holds the correct, even compression, the barrier is continuous. If it does not, the barrier can leak. This is why the crimp is treated as a critical process step, and why a consistent seal that crimps predictably matters so much. The mechanics are covered in vial crimping explained and how flip-off caps work.
The stopper’s part in closure integrity
The stopper is the barrier itself, so its compound and its fit decide whether the load the crimp applies still seals the vial months later. A stopper that is the right size but the wrong compound can pass integrity testing on the day of capping and lose sealing load over the shelf life.
Three properties of the stopper carry most of the risk:
- Fit to the neck. The stopper’s plug diameter and flange have to match the vial neck finish, defined for glass tubing vials in ISO 8362-1, and its own forms and dimensions in ISO 8362-2. A plug that is too slack leaves a path at the bore; a flange that is too thick changes the seated height the seal was sized for.
- Hardness and compression set. Rubber under constant load slowly relaxes. The more a compound takes a permanent set, the less force the stopper pushes back against the glass and the seal over time, which is why the residual sealing force measured after capping is worth tracking on stability, not only at release.
- Behaviour after puncture. On a multi-dose vial the stopper has to close the needle track after each withdrawal. Self-sealing and penetrability are functional properties evaluated under USP <382>, and in Europe under Ph. Eur. 3.2.9.
For freeze-dried products the stopper also has to seat correctly from a half-seated position at the end of the drying cycle, using a lyophilisation design with legs or slots covered by ISO 8362-5. Matching a stopper to its seal is set out in pairing the rubber stopper and aluminium seal.
What the seal itself contributes to integrity
The seal contributes four measurable things to closure integrity: crimp geometry, aluminium gauge, dimensional consistency from piece to piece, and freedom from particles and coating debris. None of them proves integrity on its own, because integrity is a property of the assembled package, but each of them is a variable the filler cannot control and the seal maker can.
- Crimp geometry. The skirt has to be long enough and formed so that it rolls cleanly under the vial neck flange without folding, tearing or springing back. Skirt length and the inner aluminium height are drawing-controlled dimensions, for example 7.37 to 7.62 mm of inner aluminium height on a 20 mm flip-off seal, because they set how much metal is available to form the roll.
- Aluminium gauge. Too thin and the metal deforms without holding the stopper down; too thick and the capping head has to work against it, which raises the risk of over-crimping the stopper or chipping the glass. Gauge is specified per size: 0.16 to 0.20 mm at 13 and 20 mm, 0.17 to 0.23 mm at 28 mm, 0.21 to 0.25 mm at 32 mm and 0.20 to 0.25 mm at 34 mm, all in AA8011 alloy.
- Dimensional consistency. A capping head is set once for a lot. If seal diameter, skirt height or gauge drifts within that lot, the finished crimp drifts with it, so compression varies vial to vial and integrity varies with it. Consistency, rather than any single dimension, is what makes a validated crimp reproducible.
- Cleanliness. Loose particles or lacquer debris on the inside of a skirt sit directly on the crimp interface. Autofits seals are washed in a fully automated line, and every seal passes 100% high-speed camera inspection before packing, with AQL set at critical nil, major not more than 2.5% and minor not more than 4%.
These four properties are what a supplier’s specification and a filler’s incoming-goods check should agree on. The seal’s contribution is to make sure the crimp the filler validated is the crimp they get on every vial of the run.
What integrity means when you specify a closure
To get closure integrity you specify the vial, the stopper, the seal and the capping settings as one system, then prove the combination by testing; specifying each part on its own and testing afterwards is how integrity failures reach stability.
| Element | What to specify | Why it matters for integrity |
|---|---|---|
| Vial | Neck finish and nominal size to ISO 8362-1 | Sets the flange the seal rolls under and the bore the stopper seals against |
| Stopper | Nominal size, design (standard or lyophilisation), named compound, and the chapters it is qualified to (USP <381>, USP <382>, Ph. Eur. 3.2.9) | The compound decides retained sealing force; the design decides how it seats |
| Seal | Same nominal size, family and top design, and the drawing dimensions: inner diameter, skirt or inner aluminium height, gauge | Sets how much metal forms the crimp and how consistently it forms |
| Form of supply | Regular, Ready-to-Sterilize or Ready-to-Use | Decides how much handling, and particle risk, sits between the seal and the crimp |
| Capping settings | Capping head pressure or crimp setting, established on the actual stopper and seal lot, with residual seal force checked | Converts the components into a compressed barrier; must be re-verified after a component change |
| Verification | CCIT method, its detection limit and when it is run (development, stability, routine) | Integrity is only claimed once it is shown for this combination |
| Change control | Notice before any change to stopper compound, seal dimensions or vial source | A change in any one part can move the crimp outside the validated window |
The destination page for choosing that combination end to end is vial closures, which covers the stopper, seal and vial neck as one specification. If the product is freeze-dried, the same table applies with a lyophilisation stopper and the capping step moved to after the drying cycle, as described for lyophilised products.
Specifications that affect the crimp
Drawing-controlled dimensions for the seals that form the crimp, from the Autofits engineering drawings. The nominal size must match the vial neck finish under ISO 8362-1 and the stopper of the same nominal diameter.
| Size and family | Inner Ø aluminium (D1) | Inner aluminium height | Total seal height | Aluminium thickness | Bridges or fins |
|---|---|---|---|---|---|
| 13 mm FlipTop Optima flip-off | 13.36 mm (min) | 6.15 to 6.40 mm | 7.62 to 8.38 mm | 0.16 to 0.20 mm | 6 taper |
| 20 mm FlipTop Optima flip-off | 20.22 mm (min) | 7.37 to 7.62 mm | 9.02 to 9.91 mm | 0.16 to 0.20 mm | 6 taper |
| 28 mm FlipTop Optima flip-off | 27.60 to 28.20 mm | 8.70 to 9.30 mm | 11.06 to 12.06 mm | 0.17 to 0.23 mm | 8 |
| 32 mm FlipTop Optima flip-off | 32.10 to 32.90 mm | On request | 14.30 to 15.50 mm | 0.21 to 0.25 mm | 12 taper |
| 34 mm FlipTop Optima flip-off | 33.60 to 34.00 mm | On request | 15.00 to 16.00 mm | 0.20 to 0.25 mm | 8 taper |
| 20 mm tear-off, all-aluminium | 20.00 to 20.60 mm | On request | 7.40 to 8.00 mm | 0.16 to 0.20 mm | 2 |
| 20 mm tear-down, all-aluminium | 20.50 to 20.70 mm | 7.50 to 8.50 mm | 7.50 to 8.50 mm | 0.18 to 0.22 mm | 2 taper |
| 32 mm tear-down, aluminium-plastic | 32.40 to 33.15 mm | 13.20 to 13.60 mm | 14.30 to 15.30 mm | 0.20 to 0.26 mm | 8 fins |
Maximum opening force is 30 N at 13 mm, 35 N at 20 mm, 35 N at 28 mm and 65 N at 32 mm, varying with the number of bridges. Opening force is a use property rather than an integrity property, but it is set by the same bridge geometry that has to survive the crimp intact. Aluminium-plastic combination caps follow ISO 8362-6; all-aluminium seals relate to ISO 8362-3. Every size is listed on the vial seals by size hub, with pages for 13 mm, 20 mm and 32 mm seals, and the flip-off range is on the FlipTop Optima page.
Forms of supply, packing and shelf life
The form of supply decides how much handling sits between the seal and the crimp, which is itself an integrity variable. Regular is the non-sterile form, for crimping outside controlled environments. Ready-to-Use seals are washed to remove particles, assembled in an ISO Class 8 cleanroom, double-lacquered, gamma or ETO sterilized and supplied double-bagged, so the outer bag is removed at entry to the aseptic area and the seals are not handled again before capping. Ready-to-Sterilize seals arrive clean and bagged for the customer’s own validated cycle. Shelf life is 3.5 years before capping for non-irradiated seals, plus 5 years after capping, and 2 years before capping for Ready-to-Use.
Standard packing is 15,000 per box at 13 mm (5,000 in each of three bags), 6,000 at 20 mm, 3,000 at 28 mm (1,500 in each of two bags) and 1,400 at 32 mm (700 in each of two bags), in a 420 × 270 × 320 mm shipper, with Tyvek bagging available. To match a seal to a validated crimp, send the vial neck finish, the qualified stopper’s reference and compound, the nominal size and the form of supply through the contact page.
What compromises closure integrity
Closure integrity is compromised whenever the stopper is not held in the right compression against the glass, whether from a poor crimp, a mismatch between components, or damage. The common causes are mechanical, and most trace back to the crimp or the fit of the parts.
- Under-crimping: too little compression leaves the stopper loose and a leak path open.
- Over-crimping: excessive force can damage the stopper or the glass finish, again opening a path.
- Component mismatch: a stopper, vial neck and seal that are not the same size or finish will not seat correctly.
- Stopper relaxation: a compound with high compression set loses sealing force over time, so a vial that passed at release can fail on stability.
- Dimensional variation in the seal: an inconsistent seal crimps unevenly, so integrity varies vial to vial.
- Damage or stress: rough handling, or freeze-thaw stress in the cold chain, can strain the seal-stopper interface, as discussed in vial closure for cold-chain drugs.
Because these are physical, they are managed by controlling the crimp, matching the components, choosing the stopper compound deliberately, and using dimensionally consistent seals.
How vial closure integrity is tested
Vial closure integrity is tested using container closure integrity testing (CCIT) methods, chosen and validated within the framework of USP <1207>. The chapter groups methods into deterministic (physical, quantitative) and probabilistic (population-based) approaches, and favours deterministic methods where possible.
- Deterministic methods measure a physical quantity linked to a leak, for example vacuum or pressure decay, helium mass-spectrometry leak testing, high-voltage leak detection, or headspace analysis on a lyophilised product stoppered under vacuum. They give a quantitative, reproducible result.
- Probabilistic methods (such as dye ingress or microbial ingress) give a pass or fail based on probability across a population; they are still used but are less favoured for routine confirmation.
- Method selection and validation are driven by the product, the package and the leak size that matters for sterility, which is what USP <1207> frames.
The full method landscape and how it is applied is covered on the container closure integrity testing page and the USP <1207> page. Integrity testing is used in development, on stability, and to confirm the closure process is under control. In the US, FDA guidance allows container closure integrity testing in place of sterility testing as part of the stability protocol for sterile products.
How this works in practice at Autofits
Autofits makes the seal whose crimp maintains closure integrity, not the stopper under it, and controls the variables on the seal’s side: dimensional consistency and cleanliness. The seal is matched to the stopper the customer has qualified with its own closure supplier, at the same nominal neck finish. The FlipTop Optima flip-off seals are made to drawing-controlled dimensions from AA8011 aluminium (EN 15088:2005, tested to BS EN 485-2:2008) with an epoxy lacquer to 21 CFR 175.300, so they crimp evenly over the matching stopper and vial neck across a run. The polypropylene disc is moulded in house on Japanese Toyo injection machines to 21 CFR 177.1520.
Every seal is checked by 100% high-speed camera inspection, and seals are produced under an ISO 15378:2017 quality system, with ISO 9001:2015 and ISO 14001:2015 certification and Drug Master File 18100, in a 75,000 sq ft Nashik facility with an ISO Class 8 cleanroom. Components are BSE/TSE-free to EMEA/410/01 rev. 3 with heavy metals held to a maximum 100 ppm total. Consistent components do not by themselves prove integrity, which is a package property the filler demonstrates by testing, but a seal held to its drawing removes a main source of variation, so the crimp the customer validated on its own stopper and vial produces a reliable barrier vial after vial.
Frequently asked questions
What is vial closure integrity?
Vial closure integrity, or container closure integrity, is the ability of a sealed vial to keep its contents in and keep contaminants and microorganisms out for the whole shelf life. It is achieved when the rubber stopper is held compressed against the glass by a correctly crimped aluminium seal, forming a continuous barrier with no leak path. It is a property of the whole package, not just of being closed.
Why does the crimp matter for closure integrity?
The crimp matters because it holds the rubber stopper compressed against the glass, and that compression is what seals the vial. The elastomeric stopper fills the microscopic gaps at the glass interface only when held under the right compression. If the crimp is too loose the barrier leaks, and if it is too tight it can damage the stopper or glass, so the crimp is a critical step in achieving integrity.
Does the stopper affect container closure integrity?
Yes. The stopper is the barrier, so its fit to the vial neck, its compound and its behaviour after puncture all affect integrity. A compound with high compression set relaxes under the crimp and loses sealing force over the shelf life, so the stopper compound should be named in the specification and tested with the seal and vial it will be used with.
What does the aluminium seal contribute to closure integrity?
The seal contributes crimp geometry, aluminium gauge, piece-to-piece dimensional consistency and cleanliness. The skirt has to roll cleanly under the neck flange, and the gauge is set per size, from 0.16 to 0.20 mm at 13 and 20 mm up to 0.21 to 0.25 mm at 32 mm. Consistency matters most, because a capping head is set once for a lot, so drift in diameter, skirt height or gauge shows up as variation in the finished crimp.
What do you need to specify for vial closure integrity?
Specify the vial neck finish, a stopper of the same nominal size with its design and named compound, a seal of the same size with its drawing dimensions and form of supply, the capping settings established on those actual components, the integrity test method and when it is run, and change control across all three parts. Integrity is claimed for that combination, not for any single part.
How is container closure integrity tested?
Container closure integrity is tested with CCIT methods selected and validated within the framework of USP <1207>. Deterministic methods, such as vacuum or pressure decay, helium leak testing and high-voltage leak detection, measure a physical quantity linked to a leak and are favoured for their reproducibility. Probabilistic methods, such as dye or microbial ingress, give a population-based pass or fail. The method is chosen for the product and the leak size that matters for sterility.
What is the difference between USP <1207> and CCIT?
USP <1207> is the guidance chapter that frames how container closure integrity is evaluated for sterile products, including how methods are classified and validated. CCIT, container closure integrity testing, is the set of physical test methods used to actually demonstrate integrity. In short, USP <1207> is the framework and CCIT is the testing carried out within it.
Does a consistent seal guarantee closure integrity?
No single component guarantees integrity, because integrity is a property of the assembled package that the filler must demonstrate by testing. However, a dimensionally consistent, clean seal removes one of the main sources of variation in the crimp, so the customer’s validated capping process can produce a reliable barrier vial after vial. The vial, stopper and seal must all be matched and correctly assembled.
Related reading
- Vial closures: stopper, seal and neck specified together
- Elastomeric closure: definition
- Container closure integrity testing (CCIT)
- USP <1207>: package integrity evaluation for sterile products
- Vial crimping explained
- The vial fill-finish process
- FlipTop Optima flip-off seals, all five sizes
Sources
- USP-NF: General Chapter <1207>, Package Integrity Evaluation, Sterile Products (https://www.uspnf.com/)
- US FDA: Guidance, Container and Closure System Integrity Testing in Lieu of Sterility Testing as a Component of the Stability Protocol for Sterile Products (https://www.fda.gov/regulatory-information/search-fda-guidance-documents)
- ISO: ISO 8362-1:2018, Injection containers and accessories, Part 1: Injection vials made of glass tubing (https://www.iso.org/standard/74398.html)
- ISO: ISO 8362-2:2024, Injection containers and accessories, Part 2: Closures for injection vials (https://www.iso.org/standard/87251.html)
- ISO: ISO 8362-5:2016, Injection containers and accessories, Part 5: Freeze drying closures for injection vials (https://www.iso.org/standard/65448.html)
- ISO: ISO 8362-6:2010, Injection containers and accessories, Part 6: Caps made of aluminium-plastics combinations for injection vials (https://www.iso.org/standard/52806.html)
- Autofits FlipTop Seals dossier and engineering drawings
*Last updated: 2026-09-15. This article is general technical information, not regulatory or compliance advice; confirm current standard editions and requirements with the issuing bodies.*
